
Cold Chamber Die Casting Services | Aluminum & Magnesium
Looking for elite cold chamber die casting services? We offer 400T–5000T automated cells for large structural parts, pore-free automotive casting, and Tier-1 IATF 16949 quality. Send your 3D files for an immediate DFM analysis.
Request a QuoteStop fighting subsurface porosity and volatile tool life. For 20 years on the shop floor, we have engineered automated 400T to 5000T cold chamber casting cells designed to inject flawless high-melting alloys for structural automotive components, dense EV enclosures, and heavy-duty industrial housings. Request Technical DFM & Quote
Beyond the Data Sheet: What it Takes to Cast Flawless High-Melting Alloys
If you are looking for a generic supplier to just pop out basic parts from an unmonitored machine, you are on the wrong page. Anyone can read an alloy datasheet. But when you are casting an A356 structural suspension arm that must endure extreme dynamic loads without tearing, or a massive, thin-walled EV battery housing that cannot leak a single drop of coolant, the generic approach fails.
In high pressure die casting, cold chamber manufacturing is where the physics gets brutal. High melting points mean severe thermal shock to the die steel. Shorter cycle windows mean your slow-shot and fast-shot velocity transitions must be calculated down to the millisecond to prevent pre-solidification or turbulent air entrapment in the shot sleeve. Over 20 years, we have optimized these variables not via guesswork, but through rigorous engineering data.
1. Tonnage Matrix & Robotic Automation: Our Industrial Muscle
Global buyers and Tier-1 procurement teams don’t care about vague promises; they care about machine capacity and process repeatability. Our facility in Dongguan, China leverages fully closed-loop automated cells ranging from 400T up to our massive 5000T platform designed specifically for large-scale aluminum die casting.
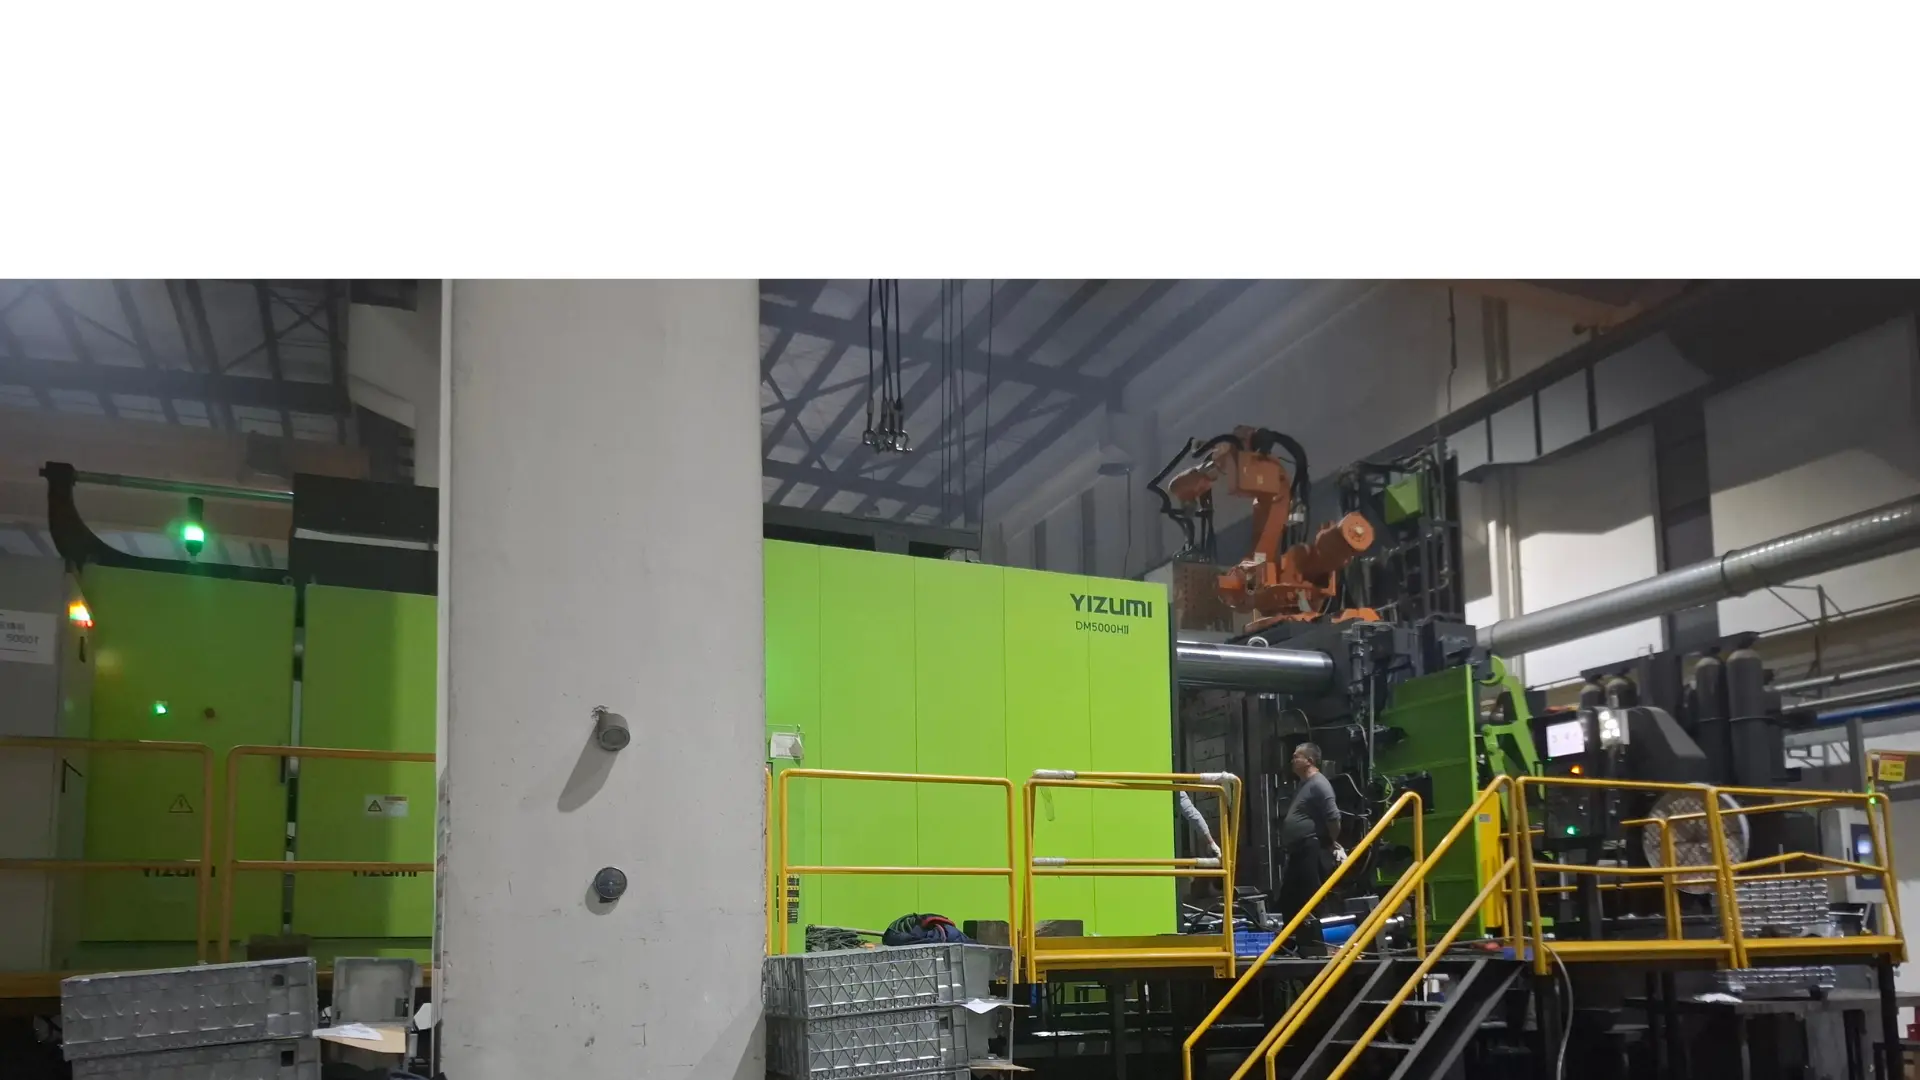 Our 5000T automated cold chamber die casting cell optimized for structural EV castings.
Every machine in our shop operates as a fully integrated robotic cell:
- Auto-Ladle Systems: Highly calibrated mechanical ladles transfer molten metal with minimal temperature drop, preventing cold shuts before the plunger moves.
- Automatic Die Spraying: Multi-axis CNC sprayers ensure absolute thermal uniformity across complex mold cores, preventing localized thermal cracking.
- Automated Robotic Extraction: High-precision robotic arms pull hot parts with zero structural distortion, transferring them directly to trimming presses.
- Vacuum-Assisted HPDC (VPDC): For safety-critical parts, we pull an ultra-high vacuum from the cavity before injection, achieving near pore-free die casting that allows for reliable structural welding and structural heat treatments.
Machine Tonnage Range Primary Alloys Processed Typical Target Applications 400T – 800T Zamak 3/5, ADC12, AZ91D Electronics brackets, medical equipment housings, connectors. 900T – 1600T A380, ADC12, AM60B Oil pans, timing gear covers, automotive powertrain parts. 2000T – 3500T A356, AM60B, AlSi10MnMg EV battery packs, cross-car beams, steering columns. 5000T Gigacasting Cell A356 (High Ductility) Integrated underbody rear structures, large liquid-cooled cooling plates.
2. Uncompromising Material Metallurgy & Process Selection
Cold chamber die casting services are mandatory for high-melting-point alloys. Why? Let’s dispel a common industry misconception: in hot chamber vs cold chamber aluminum die casting, attempting to process aluminum in a hot-chamber machine will quickly dissolve the submerged iron gooseneck, destroying your equipment and contaminating your melt. Cold chamber keeps the injection system separate, preserving metallurgical purity.
Our metallurgy lab focuses heavily on managing specialized properties for harsh mechanical environments:
- Aluminum Alloys: We run massive volumes of standard A380 properties and ADC12 properties for cost-effective mass production. However, our true specialty lies in recommending A356 over ADC12 for high-stress structural parts. A356 combined with our specialized vacuum techniques enables flawless T6 heat treatments while entirely preventing blistering.
- Magnesium Alloys: For ultra-lightweight structural shifts, we run AZ91D magnesium parts for exceptional rigidity-to-weight ratios. When impact resistance is non-negotiable (such as automotive steering wheel cores or shock towers), we execute AM60B magnesium casting due to its exceptional elongation and crashworthiness profiles.
3. Conquering Tool Life and Cracking via Rigorous DFM
The worst nightmare for a procurement manager is sourcing a cheap supplier in Asia, only to have the tool crack after 20,000 shots. Cold chamber injection causes violent thermal stress spikes. If your supplier doesn’t handle mold-flow thermal dynamics properly, your project fails.
At Alumcasting, our In-house Tooling & Mold Design Room takes control of the tool’s destiny from Day 1. Before cutting steel, we run advanced mold-flow simulations to check velocity profiles, filling behavior, and cooling layout optimization.
We do not cut corners on mold materials. We build our high-tonnage molds using supreme grades like H13 or authentic DIEVAR steel, combined with strict NADCA-standard vacuum heat treatment protocols. This guarantees our customers a stable mold life of 100,000+ shots, even under the punishing pressures of large-scale cold chamber cycles. We also analyze gating down to fractions of a millimeter, enforcing strict minimum draft angle design guidelines to prevent premature part-dragging or core wear.
4. Hardcore Verification: IATF 16949 Auditing & Lab Equipment
An expert knows that quality is not determined by an inspection at the shipping dock—it is baked into every step of the shop floor process. Our facility operates under tight IATF 16949 automotive certification standards, executing relentless in-process verification.
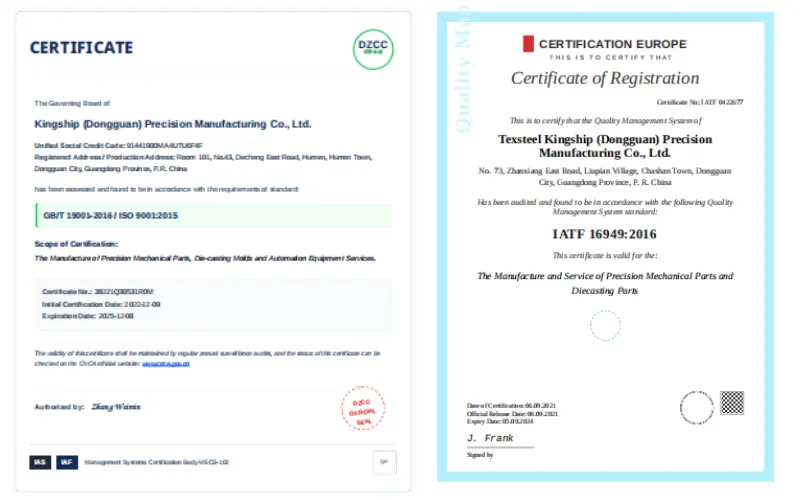 IATF 16949 Quality Audit Framework
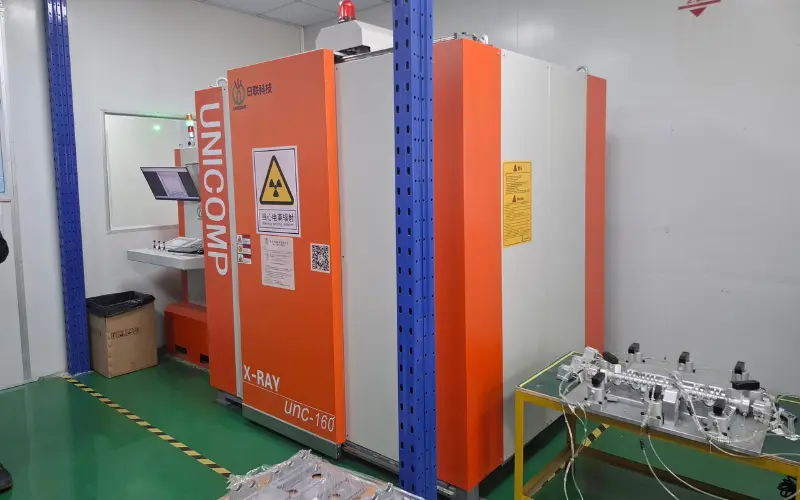 Real-Time X-Ray NDT Inspection
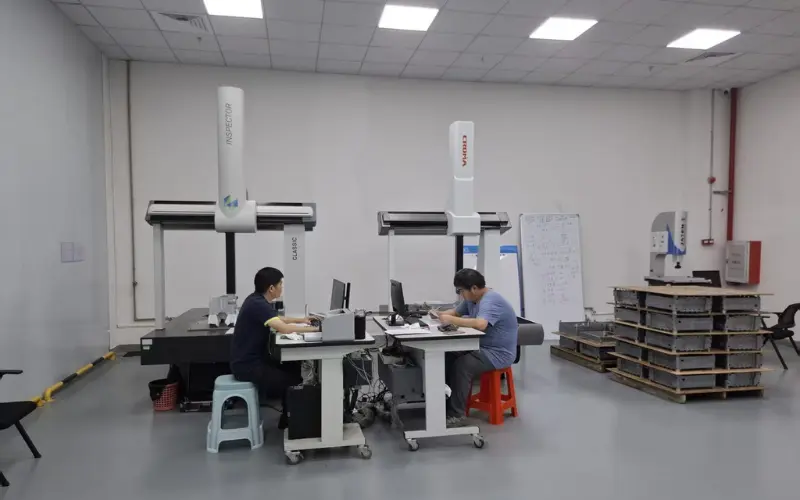 Precision CMM Metrology Lab
Our full-spectrum testing suite includes:
- X-Ray Porosity Detection: We inspect castings internally using specialized real-time X-ray equipment to ensure gas or shrinkage defects are caught before machining.
- CMM Metrology Room: Strict dimensional tolerances are verified via fully automated Coordinate Measuring Machines (CMM) to back up our micrometric print callouts.
- Spectrometer Melt Control: Every single melt heat is tested via spectrometry before injection to guarantee chemical compliance.
5. Post-Casting Secondary Operations: From Cast to Assembly
An industrial cold-chamber casting raw out of the mold is rarely a finished part. True execution requires absolute precision down the line. We provide a complete one-stop die casting, CNC machining, and surface finishing flow entirely in-house.
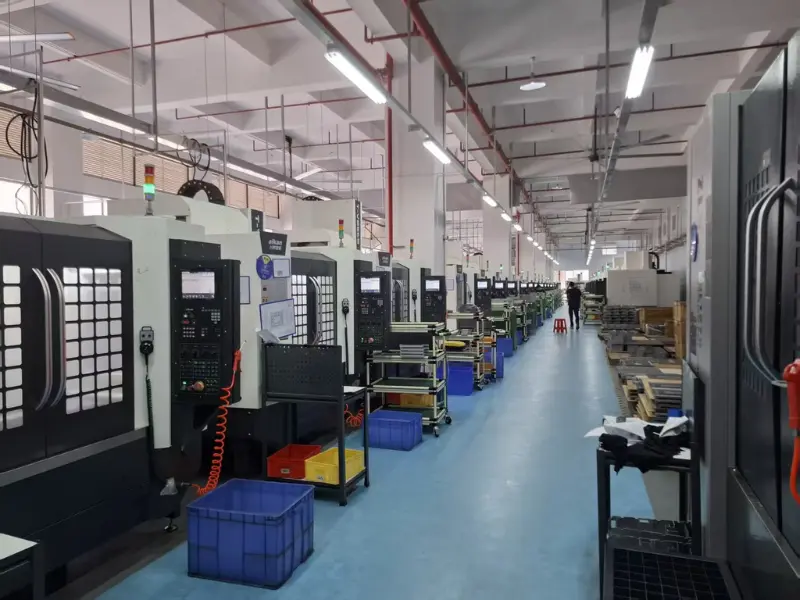 Precision 4 & 5-Axis CNC Workshop
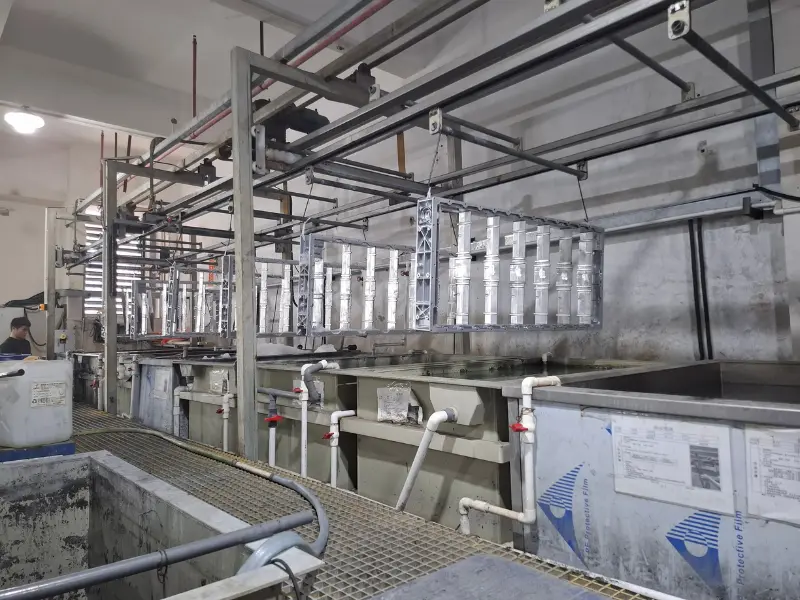 Advanced Surface Treatment Passivation
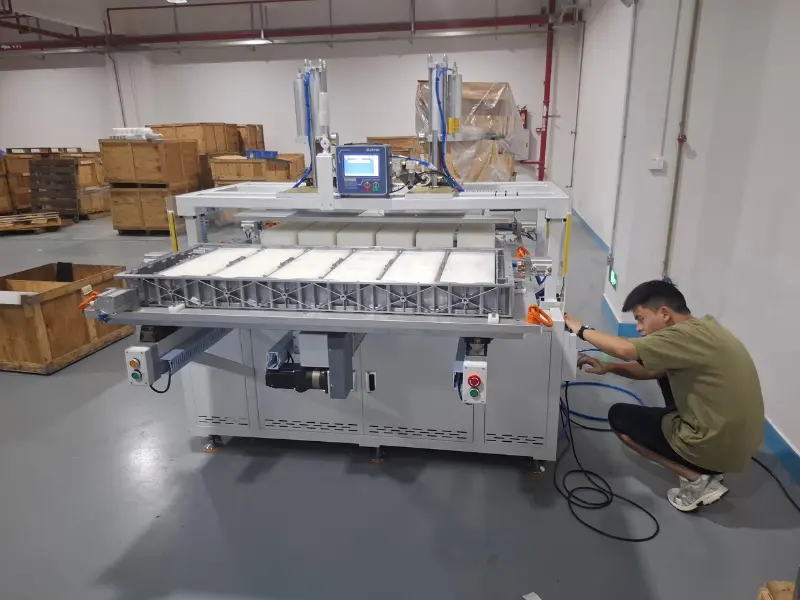 Differential Pressure Leak Testing Station
- High-Precision Machining: Our climate-controlled high-tolerance automotive CNC machining centers easily process critical datum points down to +/-0.015mm.
- Surface Modifications: From advanced MAO (Micro-Arc Oxidation) coating for magnesium protection to chromate-free SurTec 650 passivation, we protect your components against harsh environments.
- 100% Structural Leak Testing: If you are manufacturing fluid cooling loops, our automated differential air-pressure testing stations ensure every unit shipped is entirely leak-proof.
6. Seamless Logistics for Global Tier-1 Supply Chains
Based in the manufacturing core of Dalingshan and Chang’an Towns in Dongguan, our factory connects smoothly into global maritime shipping and fast air freight networks via Shenzhen and Hong Kong. Whether you need structured DDP air-freight prototype shipments for engineering validation or scheduled sea containers sent straight to automotive assembly hubs in North America, Western Europe, South Korea, or Japan, our English-fluent engineering team handles the documentation, export compliance, and packaging.
Let’s Build Something Solid Together
Send your STEP/IGS 3D models and print drawings directly to our engineering desk below. Within 24 hours, our technical team will provide an initial Design for Manufacturing (DFM) review and a direct commercial quotation.
Ready to start your project?
Talk to AlumCasting engineers about your casting, machining and tooling requirements.